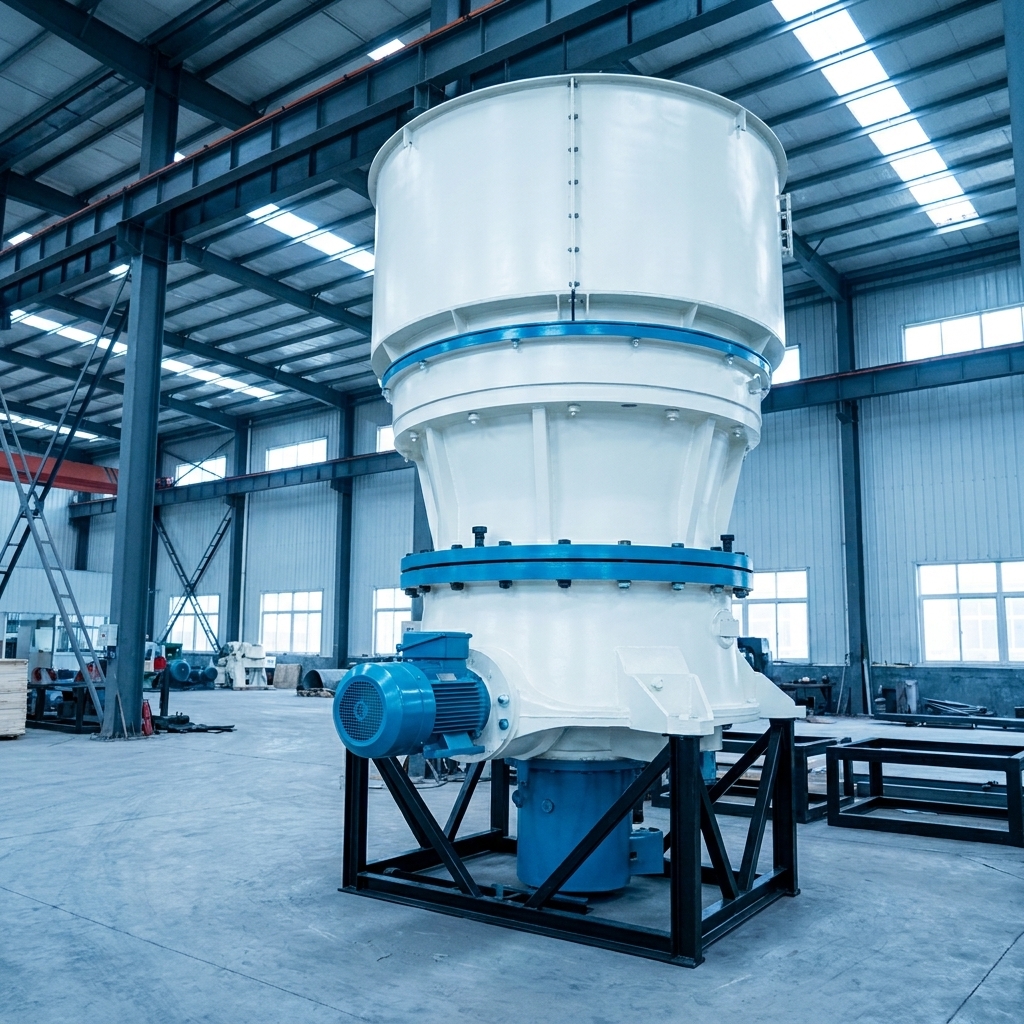
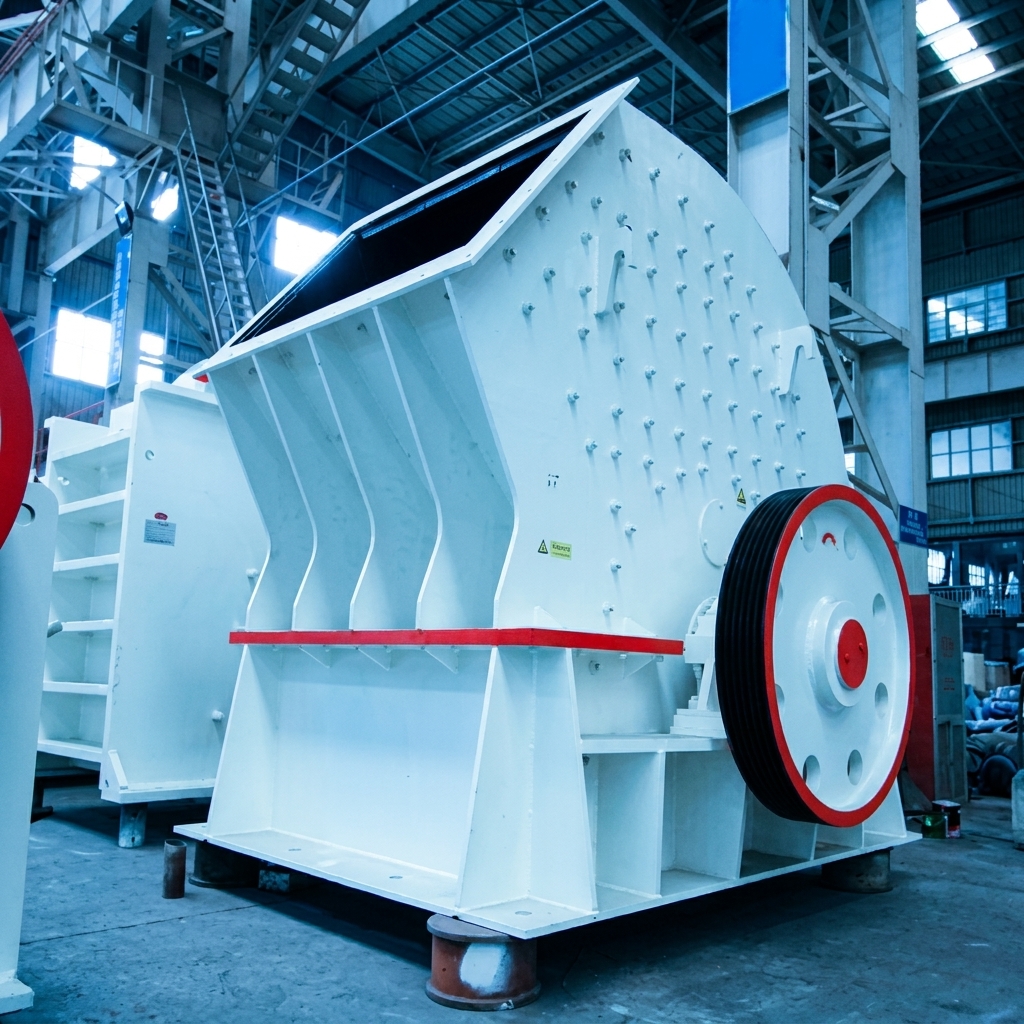
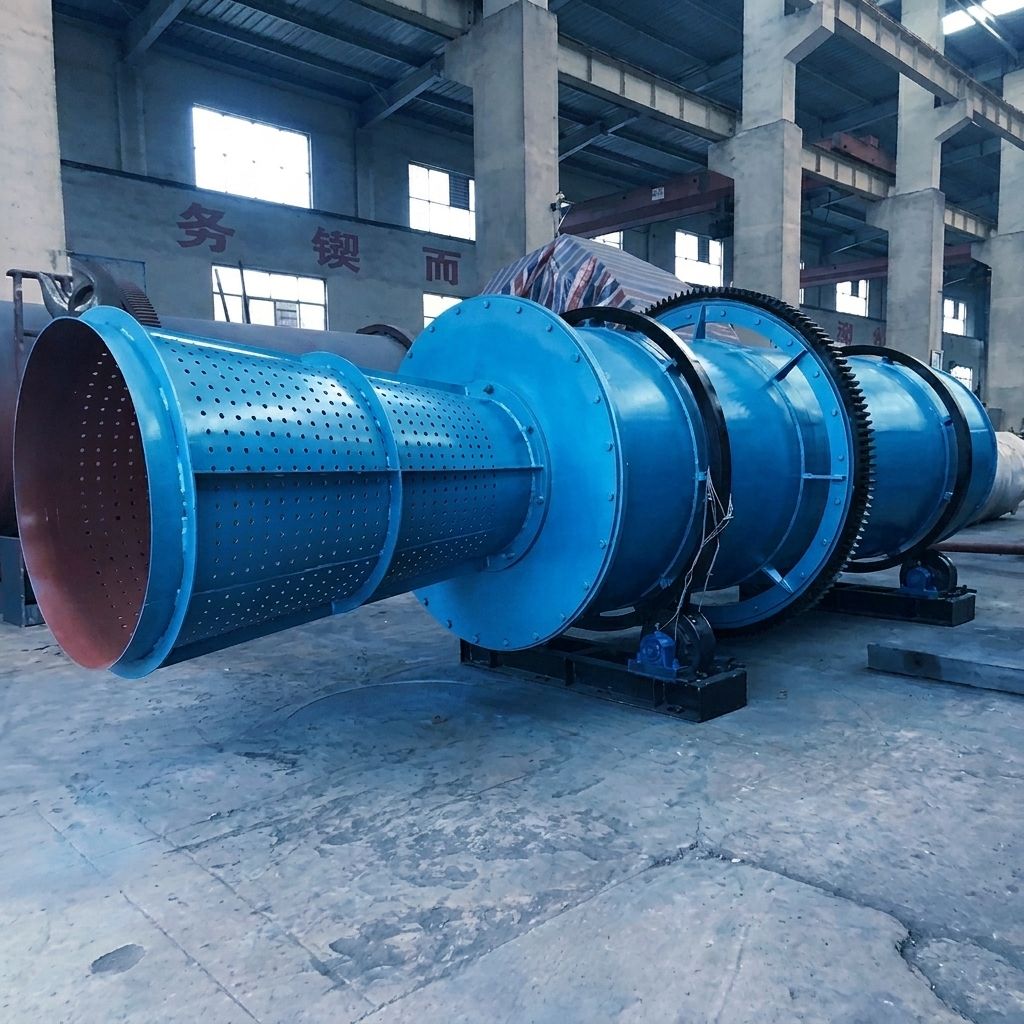
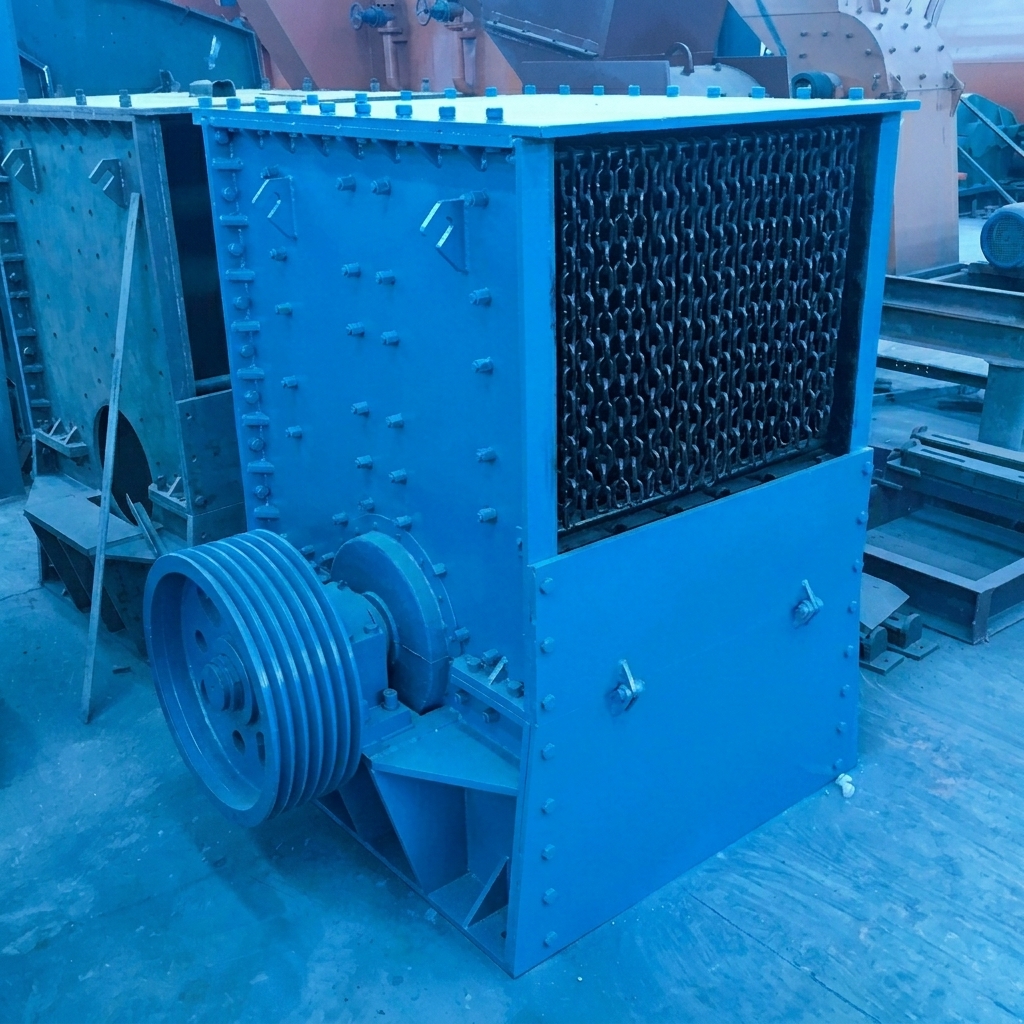
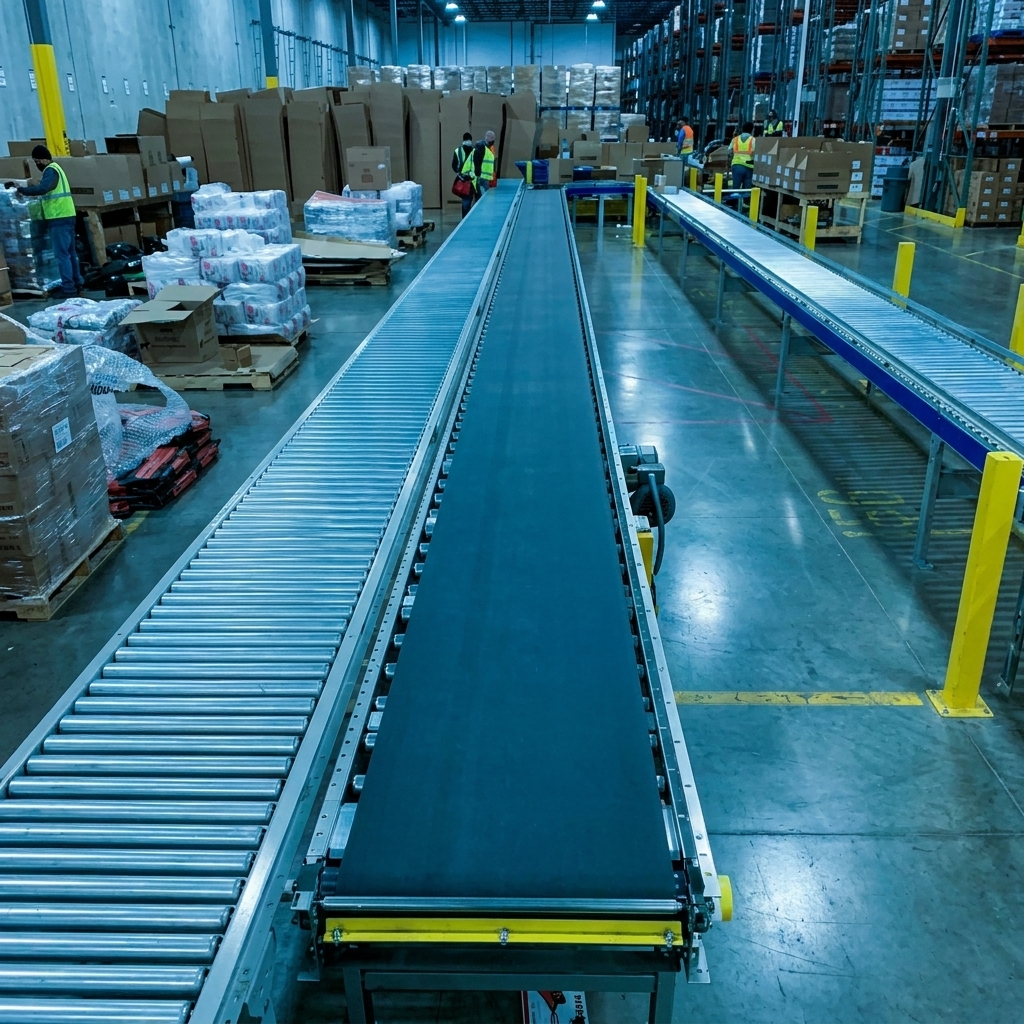
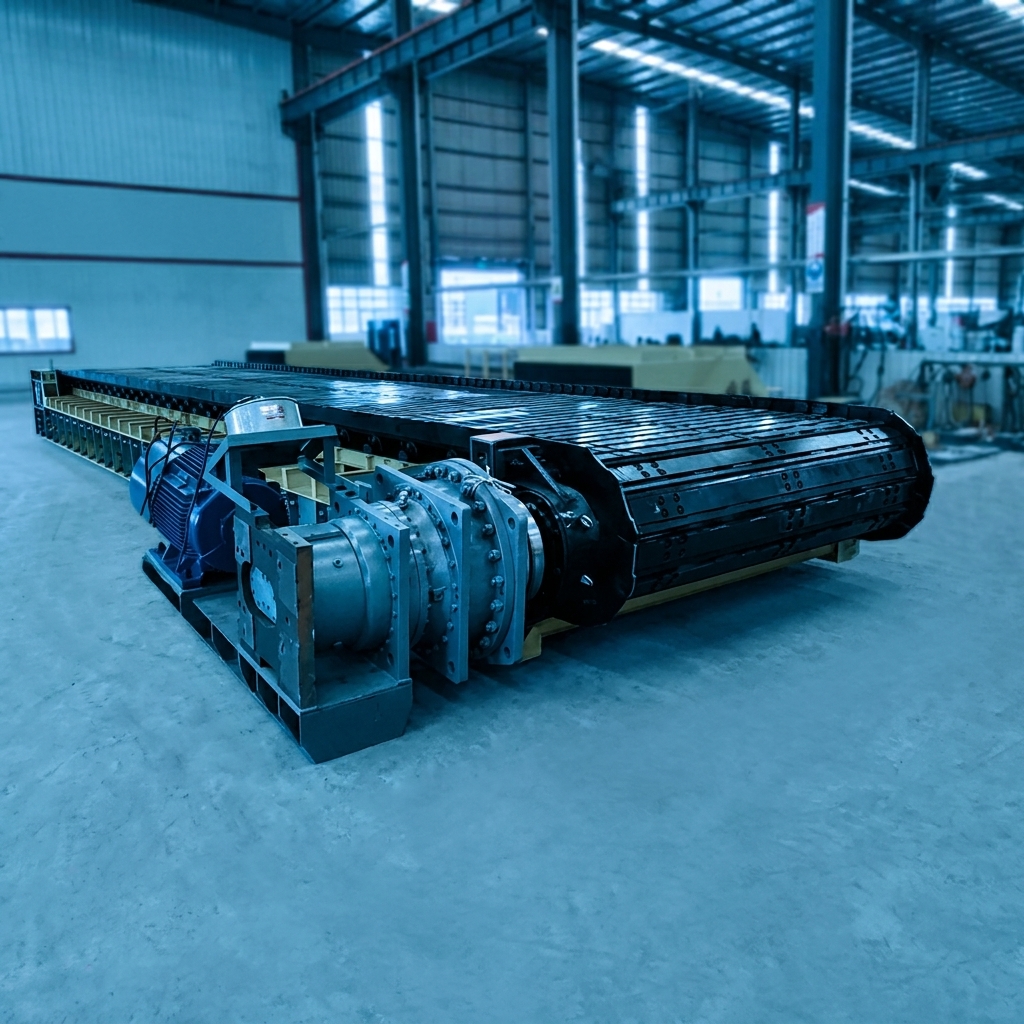
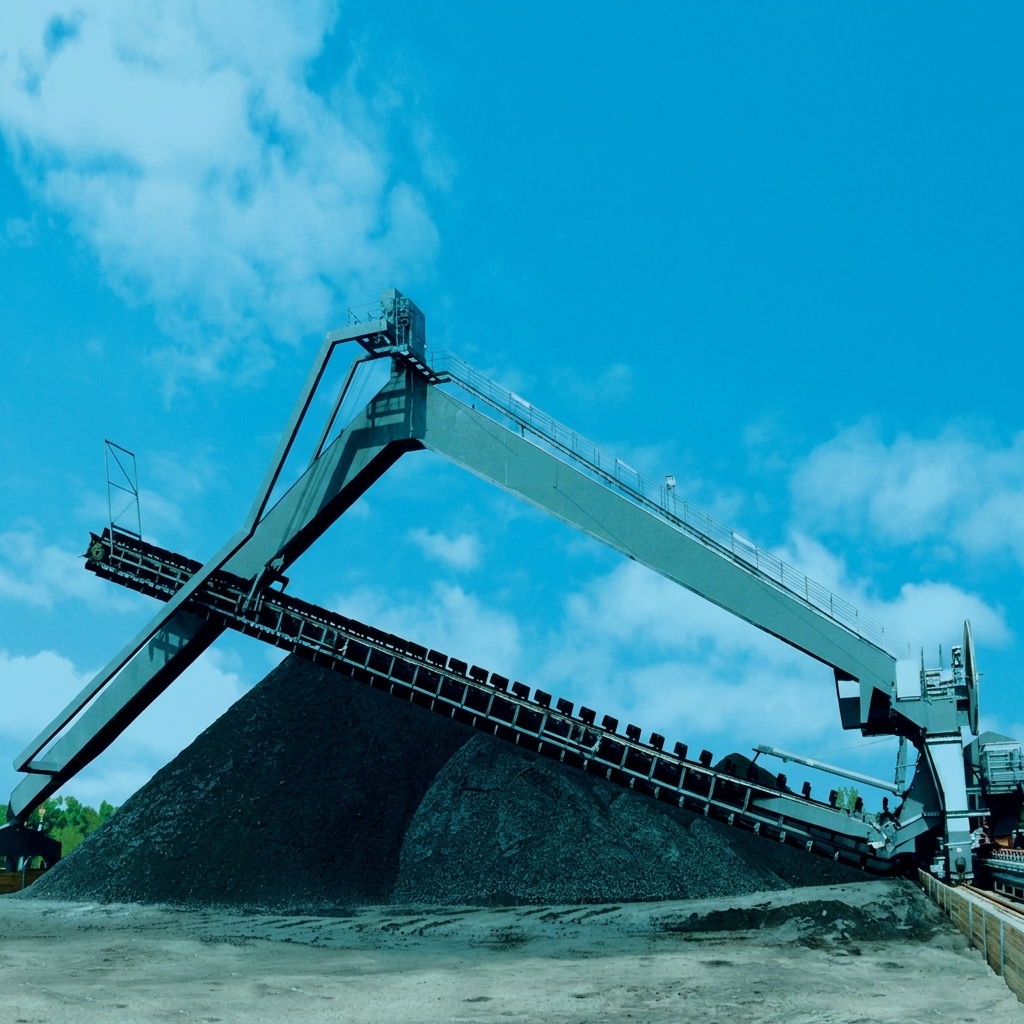
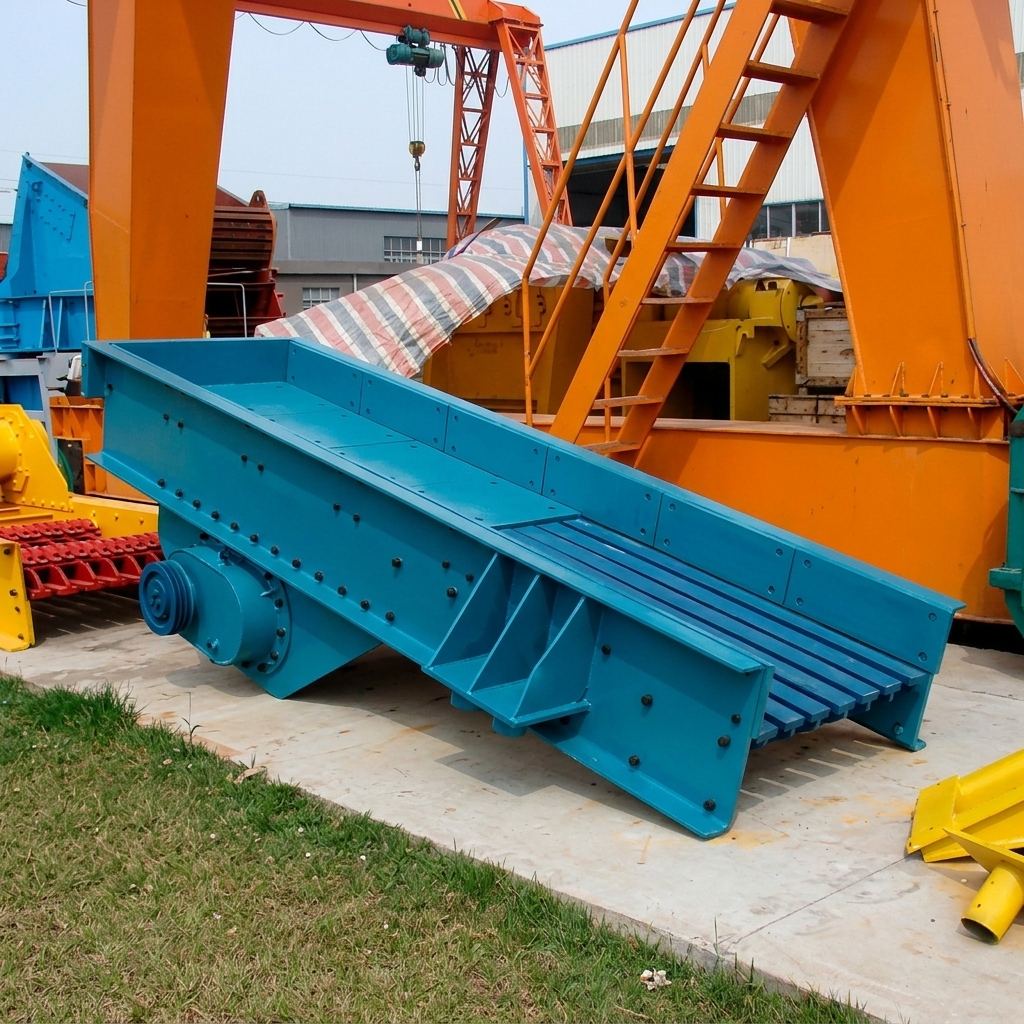
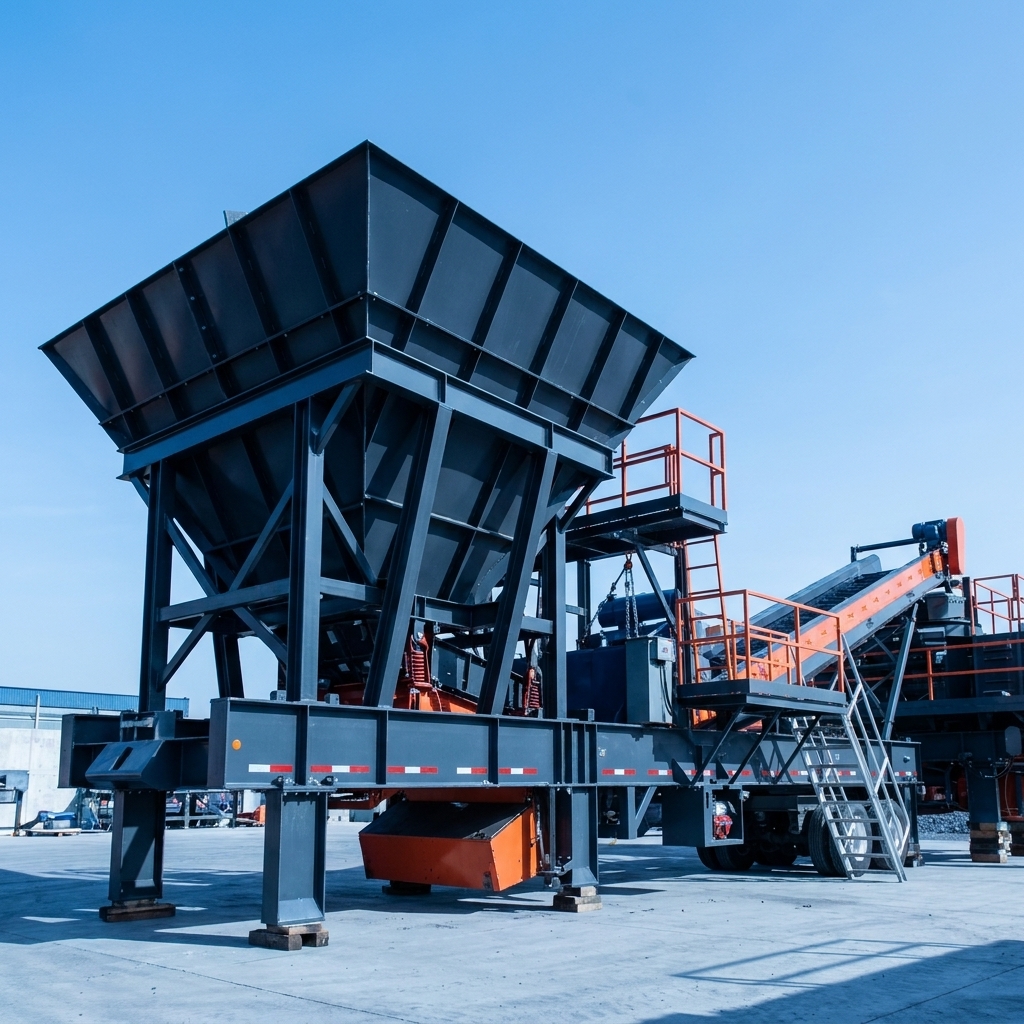
Mining demands equipment that holds up under conditions most industrial suppliers design around — sustained abrasion, shock loading, remote sites, and zero tolerance for unplanned downtime. Munir Associates supplies the full material flow chain for coal, salt, marble, and mineral extraction: heavy-duty conveyor systems, vibrating screens, dewatering and slurry pumps, drive chains, belt cleaning equipment, and vertical lifting components. Every product is sourced from manufacturers who engineer specifically for extractive industry, and selected against the actual operating conditions of Pakistani mining — not specified off a generic catalogue.